

A transmission tower shipment can arrive with every steel member listed on the packing list and still fail the buyer’s acceptance review.
The problem may not be visible in the steel. Material certificates may not match the fabricated members. Galvanizing reports may lack batch identification. Inspection records may reference outdated drawings. Or the supplier may have loaded the shipment before the required release was approved.
For EPC contractors and utilities, these documentation gaps can delay site receiving, construction, and contractual acceptance.
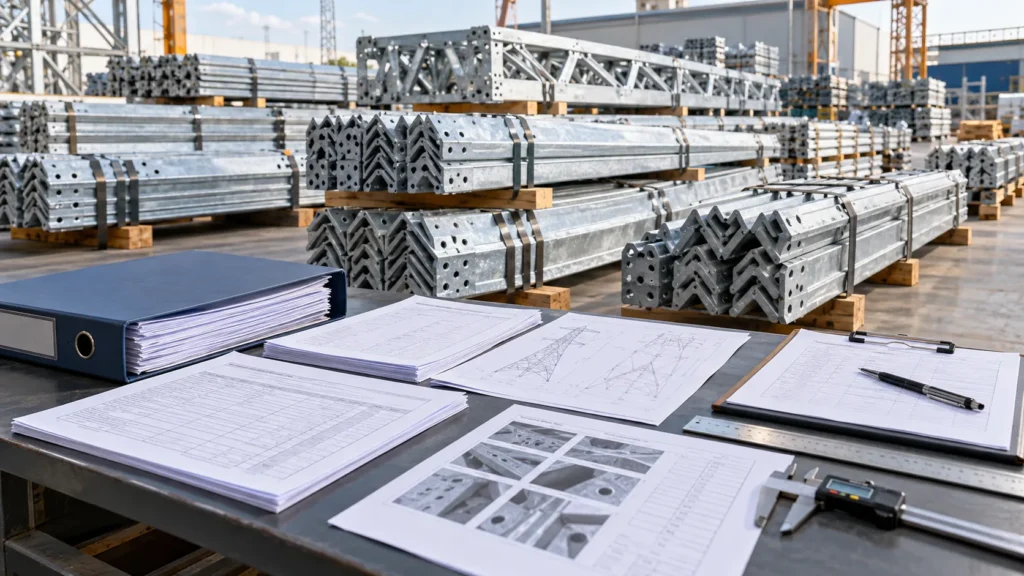
A complete shipment quality dossier should demonstrate that the delivered tower components meet the agreed requirements and can be traced through manufacturing, inspection, packing, and dispatch.
Quick Answer: What Quality Documents Should Be Included With a Tower Shipment?
Transmission tower quality documents typically include mill test certificates, material traceability records, dimensional inspection reports, galvanizing inspection reports, applicable welding and fastener certificates, final inspection reports, and shipment release documentation. Buyers should also verify approved drawing references, member identification records, packing lists, and nonconformance closure records where applicable. Trial assembly reports and third-party inspection certificates may be required by the contract or inspection and test plan (ITP). The critical requirement is traceability: the documents must correspond to the actual tower members, manufacturing batches, and packages being shipped. The final document list should be agreed upon before production.
1. Why Are Quality Documents Important for Transmission Tower Shipments?
A lattice transmission tower project may involve numerous steel angles, plates, connection components, bolts, nuts, and washers.
Once these components are fabricated, galvanized, marked, and packed, visual inspection alone cannot verify every relevant material or manufacturing characteristic.
Quality documents help buyers establish four things:
- Material conformity: Whether the specified material grades and properties are supported by relevant certificates.
- Manufacturing conformity: Whether fabrication dimensions, connections, welding, and coating have been inspected against the agreed requirements.
- Traceability: Whether manufactured components can be linked to the appropriate material and inspection records.
- Shipment release: Whether required inspections, document reviews, and approvals have been completed.
The objective is not simply to collect certificates. It is to create a verifiable record connecting the approved requirements with the physical products being delivered.
2. Which Quality Documents Should Be Included?
The following checklist provides a practical starting point for EPC procurement and pre-shipment inspection.
| Quality Document | Purpose | Applicability |
| Mill Test Certificates (MTCs) | Verify material properties and identity | Normally requested |
| Material Traceability Records | Connect material heats or lots to fabricated products | Normally requested |
| Dimensional Inspection Reports | Verify fabricated dimensions and tolerances | Normally requested |
| Galvanizing Inspection Reports | Verify coating inspection results | Galvanized components |
| Welding Quality Records | Verify applicable welded fabrication | Where welding is used |
| Fastener Certificates | Verify bolts, nuts, and washers | When supplied |
| Trial Assembly Report | Verify fit-up and connection interfaces | When specified |
| NCR and Corrective Action Records | Document deviations and their disposition | When applicable |
| Final Inspection Report | Record final product inspection status | Normally requested |
| Third-Party Inspection Report | Document independent inspection | When specified |
| Inspection Release Note | Record authorized release | Contract-dependent |
| Packing and Identification Records | Connect shipped packages to tower members | Normally requested |
The final document register should identify which records are required, who must review or approve them, and when they must be submitted.
3. Mill Test Certificates: Verifying Steel Material Conformity
Mill test certificates are fundamental documents for structural steel procurement.
Depending on the applicable material specification and certificate type, an MTC may identify the steel manufacturer, material grade, heat number, product dimensions, chemical composition, mechanical test results, and applicable standards.
What Should Buyers Check?
An EPC inspector should compare the certificate against the approved material requirements and bill of materials.
The inspector should also verify that the heat or lot number can be connected to the manufacturer’s material receiving and fabrication records.
Where EN 10204 inspection documents are specified, the required certificate type, such as 3.1 or 3.2, should be confirmed in the contract.
A mill certificate alone does not prove that the certified material was used in a particular finished tower member. That connection requires material traceability.
4. Material Traceability Records
Material traceability connects raw steel to fabricated components and their inspection records.
During tower manufacturing, original mill markings may be removed through cutting, punching, drilling, or other processing. Controlled identification transfer helps preserve the connection to the source material.
A typical traceability chain includes:
Mill Certificate → Heat or Lot Number → Material Receiving Record → Fabrication Lot → Member Identification → Packing Record
The traceability level should match the project specification.
Some projects may require individual-member identification. Others may permit controlled batch-based traceability.
Before shipment, the buyer should select sample members or controlled lots and verify that their material records can be retrieved without relying solely on verbal explanations.
5. Dimensional Inspection Reports
Dimensional inspection reports demonstrate whether fabricated tower components conform to approved drawings and specified tolerances.
Typical inspection characteristics include member length, hole diameter, hole spacing, hole position, plate dimensions, and connection geometry.
A useful report identifies the inspected member or lot, drawing revision, acceptance criteria, actual inspection results, date, and responsible inspector.
Why Do Drawing Revisions Matter?
Tower fabrication projects may involve drawing updates and engineering clarifications.
An inspection report referencing a superseded drawing may not demonstrate conformity with the current approved design.
Before shipment, compare inspection reports with the approved drawing register and confirm that relevant engineering changes have been addressed.
6. Hot-Dip Galvanizing Inspection Reports
Hot-dip galvanizing is commonly specified to protect transmission tower steelwork against corrosion.
The shipment dossier should include coating inspection records in accordance with the governing project specification.
ISO 1461 and ASTM A123/A123M are commonly referenced for applicable fabricated galvanized steel products. Their requirements are not identical, so the buyer should apply the standard specified for the project.
What Should a Galvanizing Inspection Report Include?
A useful report should identify the inspected products or batches, governing specification, coating thickness measurements, relevant visual inspection findings, repair records where applicable, and final acceptance status.
Buyers should check whether the inspection sampling, measurement locations, coating acceptance criteria, and repair methods follow the agreed requirements.
A visually uniform galvanized surface does not independently demonstrate compliance with coating thickness requirements.
7. Welding Quality Documents
Many lattice tower members are fabricated primarily through cutting, punching, drilling, and bolted connections. However, certain brackets, plates, base components, and structural assemblies may include welded joints.
Where welding is included, the project may require:
- Welding Procedure Specifications (WPS)
- Procedure Qualification Records (PQR)
- Welder qualification records
- Welding inspection reports
- Nondestructive examination reports, where specified
- Weld repair and reinspection records
The governing welding code, inspection scope, and acceptance criteria should be established before fabrication.
If the supply scope contains no welded components, welding records should not be treated as universally mandatory.
8. Fastener Certificates and Inspection Records
Bolts, nuts, and washers are essential to lattice tower connections.
Where fasteners are supplied, buyers should verify the applicable product specifications, mechanical properties, dimensions, coating requirements, and lot identification.
Relevant records may include product certificates, mechanical test reports, coating inspection records, and final inspection results.
The fastener identification and quantities should also match the approved bill of materials and packing list.
9. Trial Assembly Inspection Reports
Trial assembly helps verify whether selected fabricated tower members fit together according to the approved drawings.
Depending on the project, it may cover a complete tower, representative sections, or specific connection interfaces.
Where required, the report should identify the tower type, drawing revision, assembly scope, inspection findings, deviations, corrective actions, and acceptance status.
A successful trial assembly of one representative structure does not mean every subsequently fabricated member has been individually fit-tested.
10. Nonconformance Reports and Corrective Action Records
Nonconformance reports, or NCRs, document deviations from specified requirements.
Examples include incorrect hole positions, material discrepancies, damaged galvanizing, or dimensional deviations.
When an NCR affects components intended for shipment, the record should identify the affected products, deviation, authorized disposition, corrective work, and required reinspection.
Before shipment approval, buyers should confirm that relevant NCRs have been closed or formally accepted through an authorized concession process.
An unresolved nonconformity should not be treated as accepted simply because a final inspection report has been issued.
11. Final Inspection Reports and Shipment Release Notes
The final inspection report consolidates the acceptance status of the applicable manufacturing and inspection requirements.
It may reference material verification, dimensional inspection, galvanizing inspection, marking, packing, and outstanding quality issues.
Some projects require a separate inspection release note or certificate issued or endorsed by the purchaser or an appointed inspection agency.
A manufacturer’s internal quality approval is not automatically equivalent to the purchaser’s contractual shipment authorization.
Where inspection hold points or witness points apply, the required approvals must be completed before the relevant activities proceed.
12. How Should Quality Documents Connect to Packing Records?
One common weakness in export documentation is the separation between factory quality records and logistics records.
The quality department may use production lot numbers, while the warehouse uses bundle numbers and the freight forwarder uses container numbers.
Without controlled cross-references, buyers may struggle to identify which inspected components were actually shipped.
A practical identification chain can be structured as follows:
Approved BOM → Material Records → Fabrication and Inspection Records → Member Marks → Bundle Numbers → Packing List → Shipment Reference
For containerized shipments, container numbers and seal numbers should also be recorded in the relevant shipping documentation.
Quality and logistics documents do not need to be combined into a single file, but their references should permit reliable cross-checking.
13. Pre-Shipment Quality Document Checklist
Before authorizing shipment, EPC contractors can use the following checklist.
| Verification Item | Buyer Check |
| Document Register | Are all required records submitted? |
| Material Certificates | Do grades and material identities match requirements? |
| Material Traceability | Can relevant members or lots be linked to certificates? |
| Dimensional Reports | Are required measurements recorded and accepted? |
| Galvanizing Reports | Do results follow the governing coating specification? |
| Welding Records | Are applicable qualifications and inspections available? |
| Fastener Records | Do certificates correspond to supplied fasteners? |
| Trial Assembly | Has the specified assembly scope been accepted? |
| NCR Status | Are deviations closed or formally dispositioned? |
| Final Inspection | Are required inspections complete? |
| Hold-Point Release | Have required parties provided approval? |
| Packing Records | Do member marks, bundles, and quantities agree? |
| Shipment Authorization | Has the required release been obtained? |
A useful additional step is to sample several members or packages and trace them backward through the quality dossier.
This verifies whether the documentation system works in practice rather than merely confirming that files exist.
14. Common Quality Documentation Problems
Several preventable issues can delay shipment acceptance.
Missing material traceability: Mill certificates are supplied, but the fabricated products cannot be connected to them.
Incomplete inspection results: Reports state that products passed inspection without providing measurements required by the ITP.
Incorrect drawing revisions: Inspection records reference superseded drawings.
Unresolved NCRs: Deviations remain open or lack the necessary disposition approval.
Packing mismatches: Bundle identifiers, member quantities, and packing lists do not agree.
Late document submission: Quality records are submitted after dispatch, preventing meaningful pre-shipment review.
The most effective prevention is to establish documentation responsibilities, traceability requirements, review stages, and shipment release criteria before production begins.
15. What Should Buyers Agree With the Manufacturer Before Production?
The buyer and tower manufacturer should agree on a project-specific quality document register before fabrication.
This register should define the required records, applicable standards, inspection and testing scope, traceability level, approval responsibilities, submission schedule, and final dossier format.
The resulting package may be called a Manufacturing Record Book (MRB), Manufacturing Data Book (MDB), or final quality dossier.
The terminology matters less than the completeness, accuracy, and traceability of the records.
16. Discuss Tower Shipment Quality Requirements With HSD Steelwork
For international transmission tower projects, quality documentation requirements should be addressed during technical clarification and quotation rather than after fabrication.
Buyers can share their approved drawings, bill of materials, material specifications, galvanizing requirements, ITP, inspection hold points, document register, packing requirements, delivery destination, and shipment schedule with HSD Steelwork.
The required inspection scope, quality records, approvals, and final deliverables should be reviewed and agreed upon for each project.
Contact HSD Steelwork: https://hsdsteelwork.com
Frequently Asked Questions
1. Does every tower shipment require mill test certificates?
Mill test certificates are commonly requested for structural steel procurement. The required certificate type and traceability level depend on the contract and applicable material specifications.
2. Is a galvanizing certificate enough to prove coating quality?
Not necessarily. Buyers should verify that the documentation includes or references the required inspection results, coating acceptance criteria, and identifiable products or lots.
3. Must every transmission tower shipment include a trial assembly report?
No. Trial assembly requirements depend on the contract, tower design, project specification, and approved ITP.
4. Are third-party inspection reports mandatory?
Only when required by the contract, purchaser, applicable regulations, or approved inspection plan. Not every tower shipment requires independent third-party inspection.
5. Can a shipment be released with an open NCR?
Only where the specific disposition is permitted under the contract and all necessary approvals have been obtained. An unresolved or unauthorized nonconformity should not be treated as accepted.
6. What is the difference between a quality dossier and a packing list?
A quality dossier provides manufacturing and inspection evidence. A packing list identifies the shipped goods and packages. Their references should be linked to support traceability.